English
 Русский
 Español
 简体中文
 لالعربية
Issues encountered during the operation of steel-track shot blasting machines
release time:
2026-11-13
The operating procedure for a steel track shot blasting machine is as follows: p
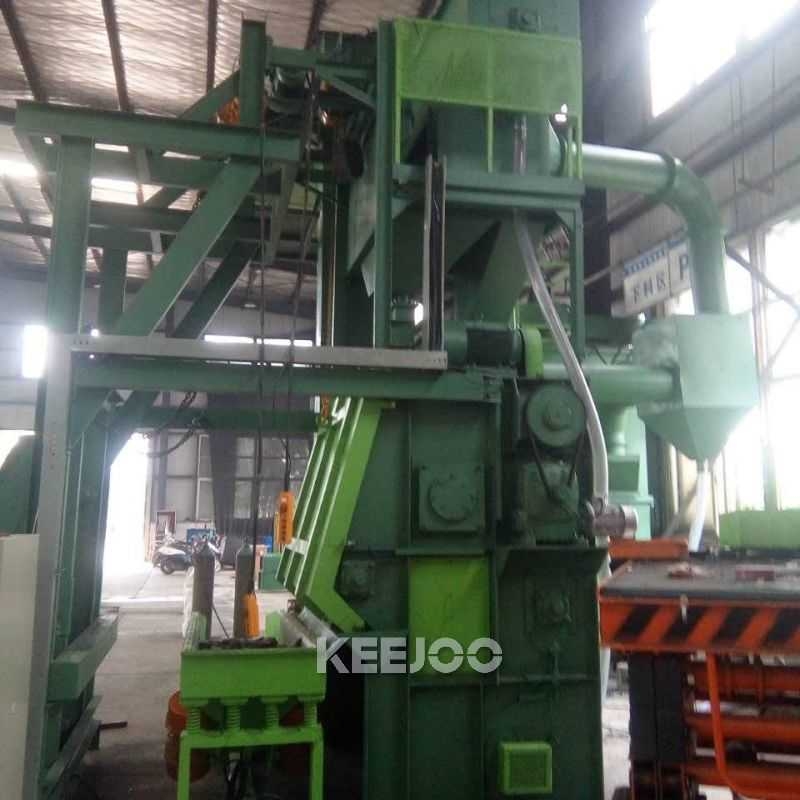
The operating procedure for a steel track shot blasting machine is as follows: pre-start inspection → loading → starting the dust collection system, elevator, and shot blasting units → shot blasting → timed sand removal → unloading. The entire process requires strict adherence to the prescribed startup and shutdown sequence, with close monitoring for any irregularities. Specific operational steps and precautions are detailed below.
Pre-startup Inspection
1. Inspection of Wear Parts: Check the condition of protective plates, rubber curtains, and tracks; replace any worn-out or damaged components promptly. Ensure that all bolts on moving parts are tight.
2. Debris Removal: Verify that no foreign objects have fallen into the machine, which could obstruct the circulation of the abrasive media (shot).
3. Abrasive Media Check: Ensure there is an adequate supply of steel shot and that it is free from contaminants such as workpiece fragments or bolts.
4. Electrical Inspection: Confirm that all motor connections and control panel wiring are secure and that all motors are in proper working order.
Boot sequence
1. No-load test machine: Start the ventilation and dust removal motors first, and then start the steel track shot blasting machine after confirming that they are working normally; do not open the iron shot control valve before starting
the shot blasting machine.
2. Confirmation of forward rotation of the crawler track: Start the forward rotation of the crawler track and observe that the crawler track moves inward; if the direction is reversed, replace the two live wires.
3. Start in seuence: start in the order of dust collector → elevator → shot blaster, conduct an idling test (about 1 hour), and check whether the no-load current, bearing temperature rise, and shot blasting amount are normal.
4. Open the pill supply gate: After the no-load condition is normal, slowly open the pill supply gate to avoid overload tripping of the motor caused by excessive pill feeding at one time.
Operational Monitoring
1. Shot Blasting Time Setting: Set the shot blasting duration based on the workpiece material and surface finish requirements. Once the set time has elapsed, a sand-clearing phase follows, during which the conveyor belt continues to rotate
forward, allowing residual steel shot to fall out of any blind recesses in the workpieces; the duration of this sand-clearing phase is adjustable.
2. Cleaning Quality Observation: Regularly inspect the cleaning quality of the workpieces. If necessary, adjust the shot projection angle (by repositioning the directional sleeve) and the speed of the conveyor belt.
3. Anomaly Monitoring: Keep a close watch for excessive vibration, unusual noises, or temperature increases in bearings and motors. If the temperature of a bearing housing exceeds 70°C, the machine must be shut down for inspection. In the event of any other abnormality, stop the machine immediately to investigate and resolve the issue.
Shutdown Procedure
1. Shut down the shot-feeding system of the steel track shot blasting machine: First, close the shot-feed pipe to stop the flow; next, turn off the shot-blasting machine motor; finally, switch off the ventilation fan.
2. Clear debris: After disconnecting the power supply, remove any debris from the screen at the bottom of the separator and clear any residual material from the conveyor belt. Daily Maintenance: Complete the handover log and perform the required maintenance for the shift.
label:
Next
related news